 English



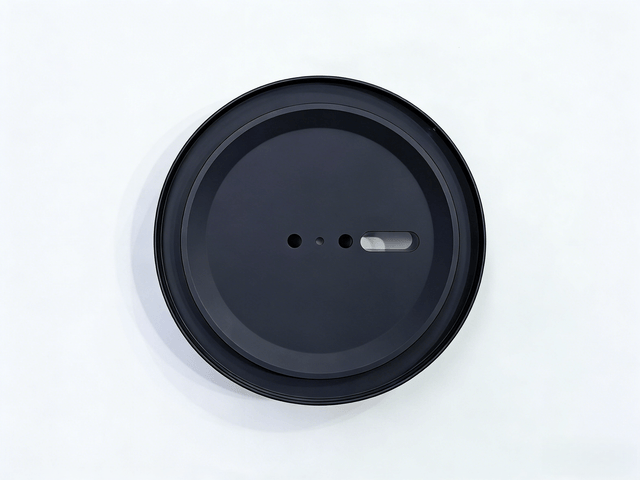
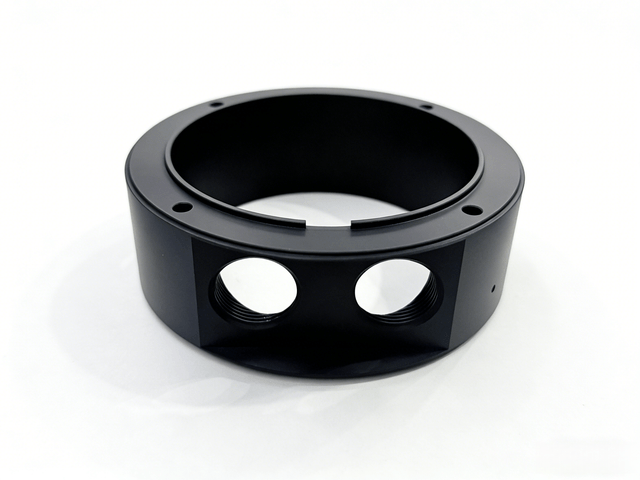
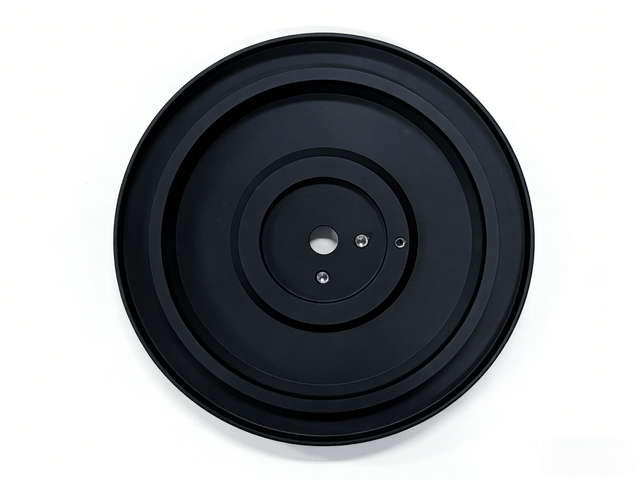
Product Description
| thing | describe |
|---|---|
| Design/Size | According to customer's drawings or samples |
| Material | Aluminum: 6061, 6063, 6082, 7075, 5052, A380, etc.
|
| process | CNC machining, turning, milling, stamping, turning, cutting, etc. |
| Delivery time | Samples usually take 3-7 working days, and mass production will be carried out according to the detailed quantity after sample approval. |
| Surface treatment | Transparent anodizing, color anodizing, chemical coating, brushing, passivation, polishing, chrome plating, sandblasting, laser engraving, zinc plating, black oxide, nickel plating, chrome plating, carburizing, heat treatment, painting |
| Test equipment | Coordinate measuring machine (CMM), 2D measuring instrument, projector, altimeter, micrometer, thread gauge, hardness tester, caliper, pin gauge, salt spray tester, concentricity measuring instrument, spectrometer. |
| Quality Management System | ISO 9001:2015
|
| application | Auto parts, machinery parts, computer parts, medical parts, home appliance parts, electrical parts, electronic product parts, electronic parts, generator parts, alternator parts, generator parts, stationery, power switches, micro switches, construction, merchandise and A/V equipment. |
| File Format | Solidworks, Pro/Engineer, CAD, PDF, JPG, DXF, IGS |
| Package | Inner plastic bag, outer standard carton, or as per customer's requirements |
| Shipping | Sea freight, air freight, international express (DHL, FedEx, TNT, UPS). |
| Serve | The professional foreign trade team provides enthusiastic and fast response services.
|
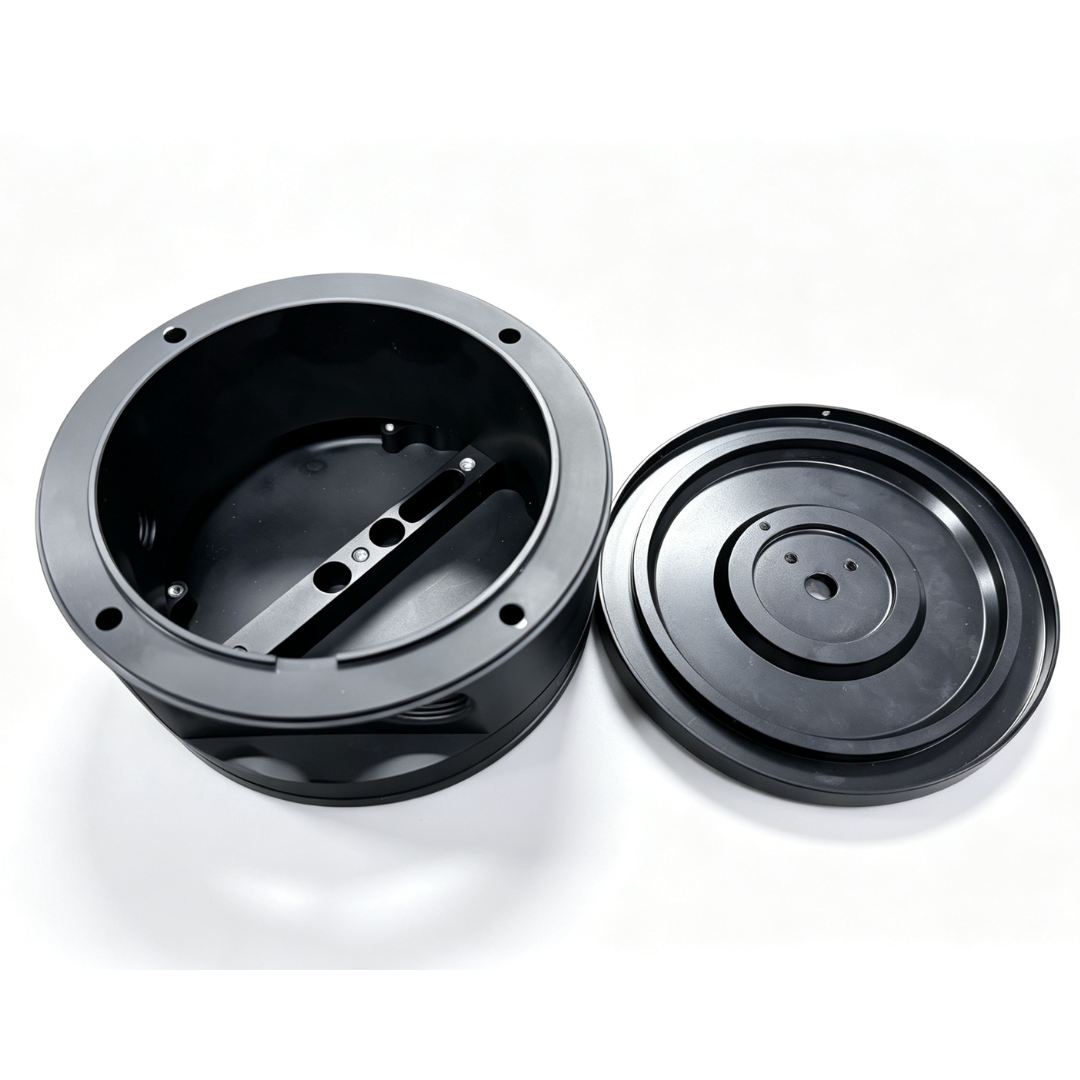
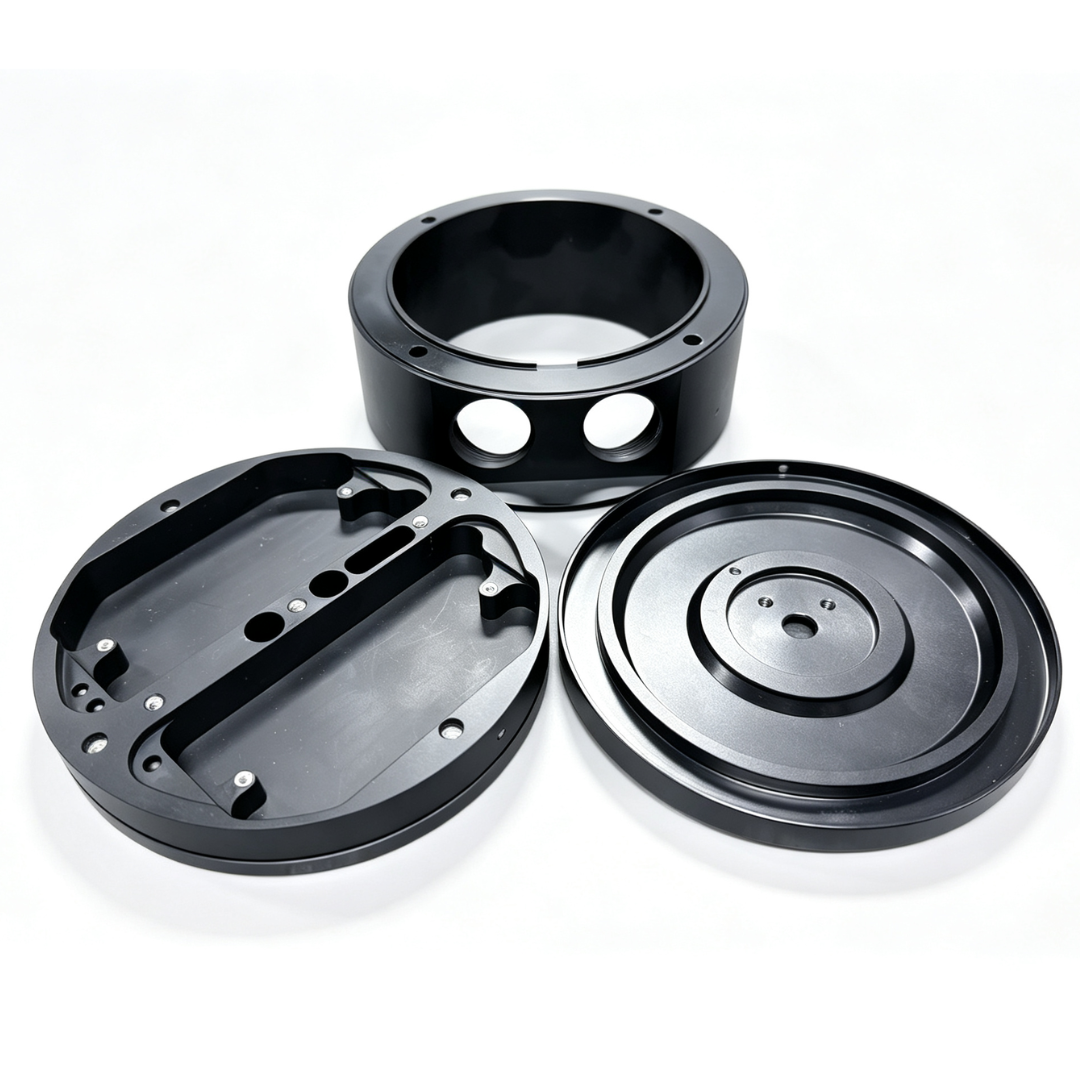
Comprehensive Product Overview
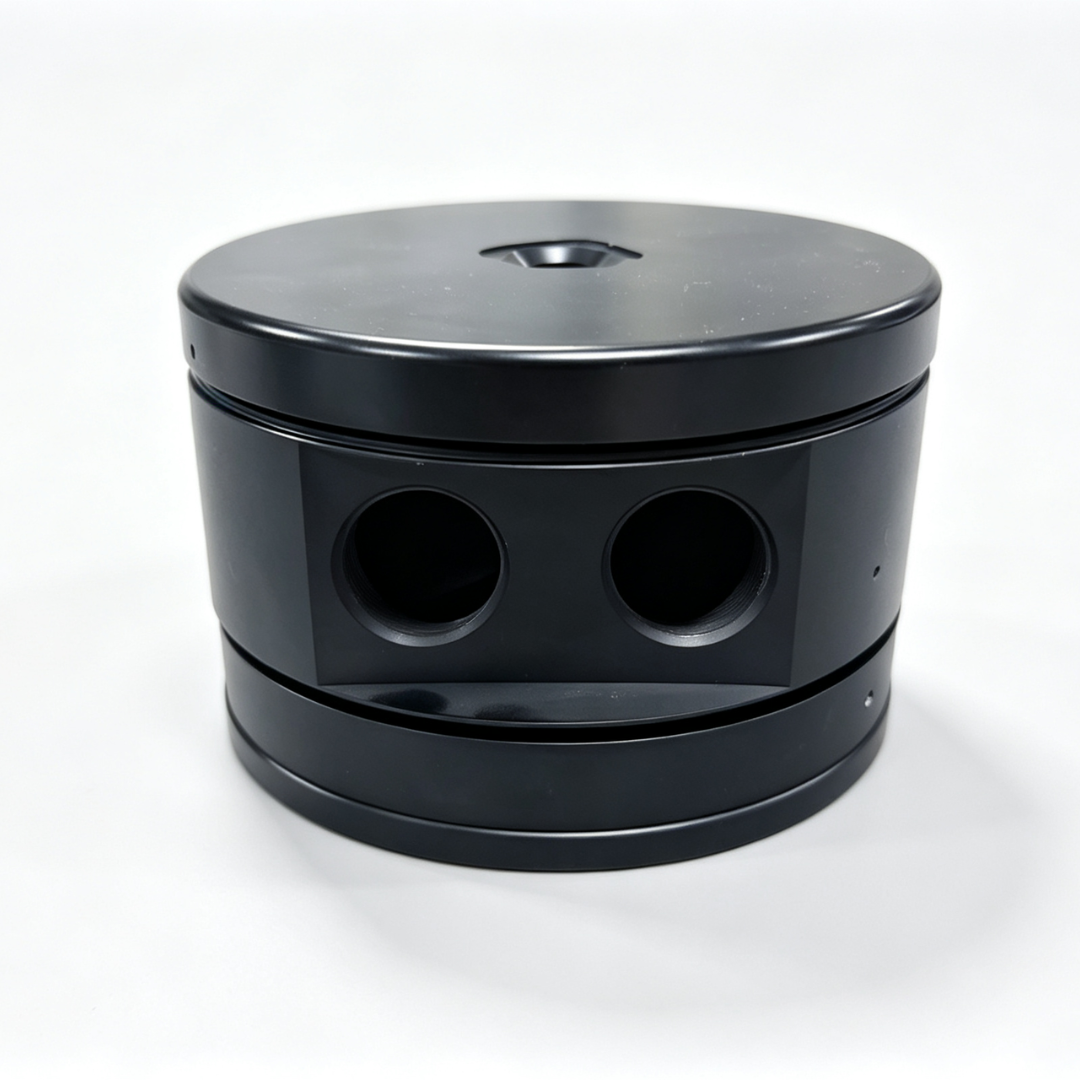
Engineered specifically to withstand the world’s most demanding marine and offshore operational conditions, this precision-machined top lid component serves as the core protective enclosure barrier for maritime signaling, deck floodlighting, and explosion-proof navigation illumination systems. Operating in oceanic environments exposes functional hardware to an unforgiving combination of corrosive airborne chloride aerosols, torrential seawater washdown, relentless solar ultraviolet radiation, and mechanical shock generated by structural hull vibrations and heavy seas.
Manufactured through subtractive multi-axis computer numerical control machining from high-integrity wrought stock, this enclosure top lid functions as an impermeable physical shield. It marries structural rigidity with an intricate concentric sealing architecture, offering industrial OEMs a turn-key enclosure closure engineered for uninterrupted dependability, absolute ingress prevention, and an extended operational lifespan in both non-hazardous and ATEX/IECEx-classified marine zones.
Material Engineering & Structural Metallurgy
-
Substrate Specification: Crafted from structural-grade EN AW 6082-T6 wrought aluminum alloy. Within maritime industrial component architecture, EN AW 6082 represents the optimal technical convergence between mechanical yield strength, weight reduction, and natural oxidation resistance.
-
Corrosion Dynamics: The underlying alloy contains a balanced composition of silicon, magnesium, and manganese. In the T6 temper condition, the material exhibits an exceptional resistance profile against intergranular corrosion and stress-corrosion cracking—a frequent failure vector in low-tier aluminum castings when subjected to the prolonged immersion and atmospheric exposure of marine boundary layers.
-
Thermal Performance and Homogeneity: Free from internal porosity, hydrogen inclusions, or micro-shrinkage voids typical of die-cast alternatives, the wrought billet material guarantees seamless thermal conductivity throughout the part body. This aids passive heat dissipation away from high-lumen enclosed solid-state luminaire modules, while preserving dimensional stability across thermal cycling ranges from sub-zero Arctic navigation temperatures up to high-ambient tropical sunlight conditions.
Rigorous Metrology & Quality Assurance Framework
-
Geometric Dimensioning & Tolerancing: Produced in strict compliance with the general tolerance classifications of ISO 2768-m, every diameter, register shoulder, counterbore, and hole pitch complies with micro-level tolerances to guarantee frictionless interchangeable assembly on customer production lines.
-
In-Process Quality Inspection Regimen:
-
First-Article Inspection (FAI): Prior to volume release, every setup undergoes exhaustive coordinate measuring machine inspection, verifying concentric alignment, thread depths, planar flatness, and concentric runout across all step features.
-
Periodic Patrol Surveillance: Production follows an uncompromising shop-floor quality protocol featuring mandatory quality checks conducted every 2.5 hours. Each audit inspects a minimum of 1 unit per machining center, expanding to a minimum of 3 units for critical operations to catch tool wear before dimensional drift can manifest.
-
Thread Integrity Validation: Axial mounting holes and radial set-screw ports (engineered for standard M3 and M4 metric fasteners) are completely gauged with certified Go/No-Go thread plug gauges, confirming precise thread engagement class, pitch diameter accuracy, and flank integrity.
-
Precision Manufacturing & Surface Finishing Workflow
-
Advanced Subtractive CNC Machining:
-
Fabricated on high-speed machining centers utilizing progressive roughing and balanced finishing passes. The strategy avoids residual stress release that often causes circular thin-rim workpieces to undergo out-of-round warping.
-
Multi-flute aluminum-specific roughing cutters swiftly establish the bulk profile, followed by specialized carbide spotting drills and precision stepped drills. These form concentric viewing apertures, wire feed-through ports, and stepped clearance bores in a single clamping reference plane, eliminating radial stack-up error.
-
Internal threads are formed using precision chipless cold-forming roll taps rather than traditional cut taps. This cold work-hardens the internal thread grain structure, ensuring superior thread flank density, zero chip debris inside blind holes, and exceptional resistance to cyclic thread stripping under high torque.
-
-
Industrial Matte Black Anodizing:
-
Before electrochemical conversion, parts undergo micro-fine media blast finishing to eradicate microscopic tool marks and produce a uniform, non-glare surface topography.
-
Components receive an industrial matte black architectural anodizing treatment. This electrochemical process converts the outer surface into an aluminum oxide ceramic shell tightly integrated with the underlying alloy.
-
Hydrothermal sealing closes the microscopic tubular pore structure, yielding outstanding surface hardness, low optical reflectivity, and the capacity to withstand over 1000 hours of continuous neutral salt spray testing without pitting, flaking, or chalking.
-
Diverse Application Scenarios
-
Commercial Marine Navigation & Signal Towers: Assembled as the primary protective upper enclosure of masthead lights, stern lanterns, and sector navigation lamps installed on container vessels, chemical tankers, and offshore tugs.
-
Offshore Oil & Gas Platforms (Explosion-Proof Enclosures): Integrated into specialized lighting fittings, hazardous junction junction-boxes, and deck beacons mounted on fixed platforms, semisubmersibles, and FPSO processing modules operating within classified zones.
-
Harbor Cranes & Marine Wind Turbines: Installed on nacelle aviation obstruction warning fixtures, quayside gantry crane lighting, and offshore substation perimeter safety floodlights where saline humidity remains consistently above 90 percent.
Key Product Advantages
-
Engineered Step-Sealing Geometry: The bottom face features precisely turned concentric steps and designated gasket-compression lands. When bolted into matching mating housings, the design provides uniform axial compression along elastomeric O-rings, achieving ingress protection ratings of IP66, IP67, and IP68.
-
Exceptional Face Planar Flatness: The controlled cutting geometry guarantees a flat seating shoulder, ensuring that high pressure washing, driving rain, and green water deck washing cannot breach the interface perimeter.
-
Vibration-Proof Retention Interface: Equipped with radial M3 set-screw ports and axial M4 threaded positions, the lid stays immovably secured to its underlying host body despite continuous structural harmonic resonance caused by shipboard marine propulsion engines or wave slams.
-
Monolithic Structural Integrity: Unlike die-cast caps that may develop micro-fissures or moisture leaks under deep hydrostatic pressure, the fully CNC-machined solid body provides high burst and impact strength, effortlessly enduring physical strikes from falling equipment or rig debris.
Measurable Customer Value
-
Elimination of Catastrophic Ingress Failures: By combining impervious alloy density with micro-precise sealing geometry, the top lid eradicates water ingress, which remains the single primary cause of optical fogging, driver burnout, and electrical shorting in offshore illumination hardware.
-
Substantial Reduction in Total Lifecycle Maintenance: Deploying maintenance crews to offshore wind turbines or ocean-going vessel masts carries significant costs and logistical complexity. This top lid component provides an extended operational design life, allowing equipment operators to bypass premature part changeouts and unplanned offshore service dispatches.
-
Elevated Architectural Aesthetic and Brand Reputation: Beyond industrial resilience, the deep, non-reflective black finish and chamfered edges deliver a premium tactile and visual aesthetic that reinforces end-user perception of structural excellence, enabling luminaire manufacturers to capture greater value in demanding global tender bids.
FAQ
Q1: What structural advantages does EN AW 6082-T6 offer over conventional die-cast aluminum for this top lid?
A1: Unlike standard aluminum die castings that inherently suffer from micro-porosity, cold shuts, and subsurface shrinkage voids—which inevitably act as capillary moisture pathways under marine humidity—solid EN AW 6082-T6 wrought alloy provides continuous structural density and uniform metallurgical grain flow when fully CNC-machined. This premium marine-grade alloy delivers exceptional yield strength, superior thermal conductivity to dissipate luminaire heat, and high immunity to stress-corrosion cracking and intergranular pitting, ensuring the enclosure endures perpetual engine harmonics, thermal shock, and green water deck slamming without micro-cracking or structural fatigue.
Q2: How does the mechanical engineering of the lid ensure an impenetrable IP67/IP68 ingress seal?
A2: Reliable watertight performance is achieved through micro-tolerance CNC turning that creates multi-tiered, self-centering circular register shoulders and dedicated O-ring containment glands. By strictly controlling face flatness and concentric runout across all step profiles, the lid delivers balanced, non-distorting compression across elastomeric gaskets when drawn tight by the precision-tapped axial M4 fasteners and radial M3 set screws; this engineered compression profile eliminates localized sealing gaps and micro-channel air paths, preventing optical lens misting, driver short-circuits, and salt-laden vapor ingress during heavy ocean storms or high-pressure sea-water washdown routines.
Q3: Can the matte black anodized surface treatment withstand prolonged UV exposure and saltwater spray offshore?
A3: Yes; before electrochemical conversion, each top lid undergoes precision media bead blasting to remove machining striations and create an isotropic matte topography, followed by an industrial-grade architectural black anodizing cycle that transforms the outer layer into an integrated, rock-hard aluminum oxide ceramic barrier. Subsequent hydrothermal sealing closes every microscopic pore to seal out airborne chlorides, allowing the finish to withstand more than 1000 hours of continuous neutral salt spray exposure without blistering, flaking, or chalking, while resisting solar UV degradation and providing an anti-glare finish essential for marine safety.
TEL: +86 187 5714 8656
Email: zhouli@chinaliqin.com
WhatsApp:+86 187 5714 8656
Website:https://www.cncliq.com/