 English





Product Description
| thing | describe |
|---|---|
| Design/Size | According to customer's drawings or samples |
| Material | Aluminum: 6061, 6063, 6082, 7075, 5052, A380, etc.
|
| process | CNC machining, turning, milling, stamping, turning, cutting, etc. |
| Delivery time | Samples usually take 3-7 working days, and mass production will be carried out according to the detailed quantity after sample approval. |
| Surface treatment | Transparent anodizing, color anodizing, chemical coating, brushing, passivation, polishing, chrome plating, sandblasting, laser engraving, zinc plating, black oxide, nickel plating, chrome plating, carburizing, heat treatment, painting |
| Test equipment | Coordinate measuring machine (CMM), 2D measuring instrument, projector, altimeter, micrometer, thread gauge, hardness tester, caliper, pin gauge, salt spray tester, concentricity measuring instrument, spectrometer. |
| Quality Management System | ISO 9001:2015
|
| application | Auto parts, machinery parts, computer parts, medical parts, home appliance parts, electrical parts, electronic product parts, electronic parts, generator parts, alternator parts, generator parts, stationery, power switches, micro switches, construction, merchandise and A/V equipment. |
| File Format | Solidworks, Pro/Engineer, CAD, PDF, JPG, DXF, IGS |
| Package | Inner plastic bag, outer standard carton, or as per customer's requirements |
| Shipping | Sea freight, air freight, international express (DHL, FedEx, TNT, UPS). |
| Serve | The professional foreign trade team provides enthusiastic and fast response services.
|
Engineering Overview & Target Application Analysis
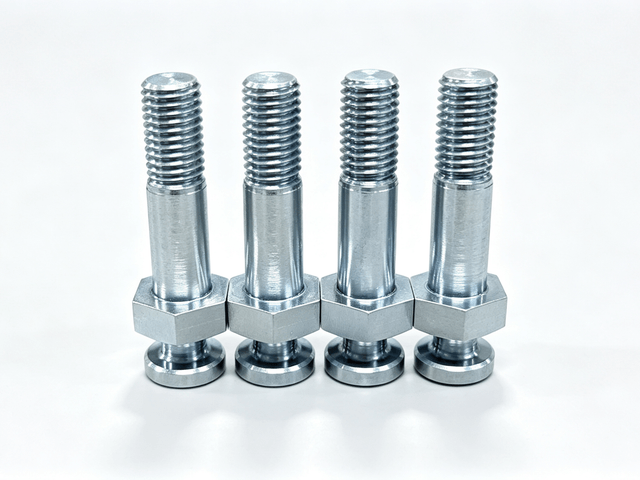
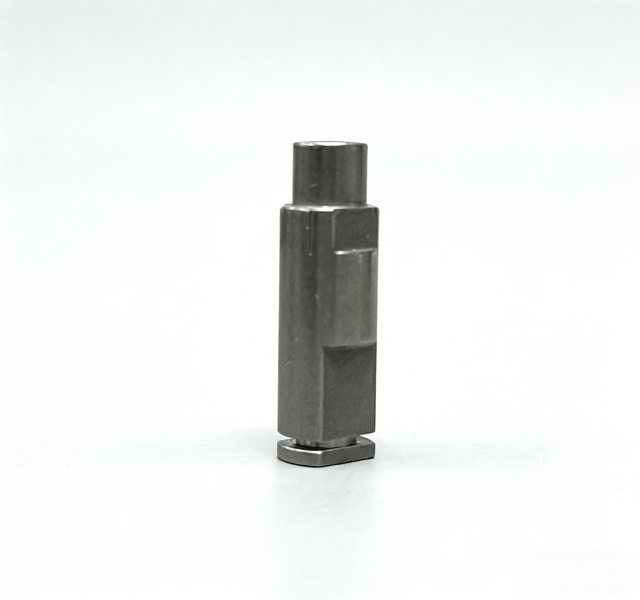
From its structural geometry and technical callouts—specifically designated as a fork support screw featuring an integral hexagonal drive collar, high-precision guide shanks, dual convex spherical surfaces with a large curvature radius, and a necked retention spool groove—this component is engineered for heavy-duty vehicle transmissions, off-highway powertrain actuators, and mobile hydraulic valve linkages.
In modern automated manual transmissions, dual-clutch gearboxes, and electro-hydraulic agricultural or construction power-shift systems, shifting forks and selector yokes must translate hydraulic or electromechanical linear force into smooth, rapid gear engagements. Standard threaded fasteners cannot satisfy these conditions because shifting mechanisms endure intense cyclic shear, continuous engine vibration, fluid immersion, and dynamic misalignments. This specialized fastener functions simultaneously as a high-strength structural anchor, a self-aligning spherical pivot interface, and a precision axial guide pin. The spherical crown and contoured neck provide a low-friction seat for shifting fork pads or pneumatic and hydraulic slave cylinder pushrods, allowing micro-angular deflection without localized stress risers or binding.
Material Science & Metallurgical Integrity
The component is machined from European standard structural alloy steel 36CrNiMo4, compliant with EN 10083 and DIN 1.6511, a premier nickel-chromium-molybdenum through-hardening grade widely recognized for critical powertrain components.
The metallurgical selection provides exceptional core hardenability, fatigue endurance, and impact toughness:
-
Chromium and Molybdenum Synergy: The combined addition of chromium and molybdenum provides deep hardenability, elevated yield strength, and remarkable temper resistance, ensuring that the bolt maintains dimensional stability under sustained operating temperatures up to 200 degrees Celsius within hot transmission fluid environments.
-
Nickel Contribution to Toughness: The presence of nickel promotes high notch toughness and fracture resistance, which prevents sudden brittle failure under abrupt impact shifts or aggressive torque shocks.
-
Microstructural Homogeneity: Supplied as hot-rolled and peeled round bar stock with an initial diameter of 20 mm, the raw material undergoes rigorous ultrasonic inspection to guarantee internal density, zero micro-porosity, and strict inclusion control.
-
Post-Heat Treatment Characteristics: Quenched and tempered prior to or after precision roughing, the alloy achieves a homogenous tempered martensitic matrix with a balanced core tensile strength exceeding 1000 MPa, an elongation rate above 11 percent, and high dynamic fatigue strength.
Manufacturing Process & Precision Engineering Route
Manufacturing this complex component requires a multi-stage CNC machining, turning, thread generation, and finishing protocol designed to achieve tight concentricity across multiple functional diameters while preserving raw material fiber orientation:
-
Precision Dual-Spindle Multi-Axis CNC Turning: Raw alloy bars are processed on multi-axis turning centers equipped with live tooling. The component requires continuous axial turning to establish the 10.2 mm guide shank, the 14.5 mm head diameter, and the critical necked spool profile in a synchronized setup, eliminating concentricity errors between the thread pitch axis and the head contours.
-
Precision Hexagon Milling (Ch 16): The integral 16 mm hexagonal driving collar is generated using synchronized polygon milling or dynamic end-milling live heads. This eliminates the structural vulnerabilities associated with welded or press-fitted assemblies, ensuring the fastener can withstand high torque transmission without rounding or shearing during robotic assembly.
-
High-Precision Spherical Profiling and Superfinishing: The specialized dual spherical surfaces—featuring an expansive R300 mm convex radius and an R2.5 mm transition fillet—are interpolated using specialized profiling inserts. The convex contact faces require a super-smooth finish with a surface roughness of Ra 2.0 or better, strictly free of witness lines, center nibs, or step marks, ensuring uniform distribution of hydraulic contact pressure and preventing seal wear in mating fork cups.
-
Thread Rolling and Transition Radii Control: The M10 thread is cold rolled rather than cut, ensuring that the metallic grain flow remains uninterrupted along the root and crest profiles. The critical thread root undercuts and transition fillets of R0.5 mm are carefully formed to relieve mechanical stress concentrations during high-cyclic vibration.
-
Surface Treatment and Corrosion Resistance: The part is finished with an engineered white galvanizing zinc electroplating layer possessing a minimum deposit thickness of 0.012 mm, or 12 microns. The coating is subjected to immediate post-plate hydrogen embrittlement relief baking, followed by a passivated sealing coat. The treated surface reliably exceeds 72 hours of neutral salt spray testing per ASTM B117 and ISO 9227 without producing red rust.
Stringent Quality Control & Dimensional Metrology
Quality assurance follows a strict automotive-grade methodology, incorporating real-time statistical process control at regular 2.5-hour intervals, initial first-piece validation, and full-dimensional final shipment screening:
-
Critical Shank Diameter: The 10.2 mm outer diameter with a tolerance of minus 0.02 mm is verified using high-precision digital micrometers to guarantee smooth sliding engagement with mating linear guide bushings.
-
Contoured Neck Thickness: The central 3.92 mm neck dimension with a tolerance of minus 0.10 mm to minus 0.15 mm and symmetrical R300 profiles are measured using digital profile projectors and optical contour testing machines to ensure faultless engagement with retaining clips and fork detents.
-
Thread Tolerancing: The M10 external thread is inspected using calibrated 6g go and no-go ring gauges before and after electroplating, ensuring rapid tool assembly while maintaining thread shear security under torque.
-
General Tolerances and Cleanliness: Non-toleranced dimensions adhere to ISO 2768-m medium machining and ISO 2768-H standards. Finished parts undergo industrial ultrasonic degreasing to ensure zero metallic burrs, chips, or residual plating salts.
Core Product Advantages & Technical Superiority
-
Dual Functional Integration: Combines an axial guide shoulder, a high-torque hex tightening drive, an external securing thread, and a self-centering spherical engagement head into a single, compact component.
-
High-Cyclic Fatigue Endurance: Through-hardened 36CrNiMo4 steel combined with cold-rolled thread roots provides superior dynamic load endurance compared to standard carbon steel fasteners.
-
Self-Aligning Kinematics: The precision R300 spherical profile accommodates angular micro-misalignments inherent to automotive linkage deflection, substantially reducing side loading and frictional wear on actuator components.
-
Fluid and Environmental Resistance: Advanced 12-micron white galvanic coating provides dependable defense against moisture, synthetic transmission oils, extreme-pressure gear lubricants, and washdown environments.
Commercial Value & Industrial Impact
Deploying this precision fork support screw delivers quantifiable operational and economic returns to tier-one automotive and industrial equipment manufacturers:
-
Enhanced Powertrain Reliability: By mitigating stress concentrations and preventing pivot-point binding, this component extends the service life of internal shift mechanisms beyond 500000 continuous engagement cycles, dramatically lowering warranty claims and field failure rates.
-
Streamlined Assembly Line Efficiency: The integrated hex flange and guide pilot facilitate rapid robotic alignment and automated torque-to-yield fastening, shortening vehicle assembly station cycle times.
-
Total Cost of Ownership Reduction: Consolidating multi-piece bushing, pin, and bolt assemblies into a single monoblock precision part eliminates secondary assembly operations, simplifies bill-of-materials management, and minimizes supply chain complexity.
FAQ
Q1: What is the mechanical function of the expansive R300 mm convex spherical face and the necked retention groove?
A: This specialized geometry provides a low-friction, self-aligning pivot interface specifically engineered to accommodate micro-angular deflections during gear shift actuation. The expansive R300 mm curvature allows shifting fork pads or hydraulic pushrods to articulate smoothly without localized edge pinching, stress risers, or mechanical binding. The precision-machined 3.92 mm neck groove serves as a locating seat for retaining snap rings, detent clips, or return springs, ensuring positive axial retention while preserving dynamic rotational freedom. Machining both features in a single CNC setup guarantees high concentricity and a smooth surface finish under Ra 2.0 microns.
Q2: Why is 36CrNiMo4 alloy steel selected for this component, and how does the manufacturing process ensure thread fatigue endurance?
A: 36CrNiMo4 (EN 10083 / DIN 1.6511) offers an optimal balance of through-hardenability, core tensile strength exceeding 1000 MPa, and high notch impact toughness, preventing brittle fracture and micro-fatigue failures in severe transmission environments. To maximize fatigue life, the M10 external thread is produced via precision cold thread rolling rather than single-point cutting. Cold forming preserves uninterrupted metallic grain flow along the thread flank and root, introducing beneficial residual compressive stresses that, combined with the R0.5 mm stress-relief root radius, prevent fatigue crack initiation and support an operating lifespan beyond 500000 dynamic cycles.
Q3: How does the minimum 0.012 mm (12-micron) white galvanizing coating impact the tight tolerances of the 10.2 mm guide shank and M10 thread?
A: Dimensional accuracy is maintained through engineered pre-plating tolerance compensation during the CNC turning and thread rolling operations. The 10.2 mm outer diameter (toleranced to minus 0.02 mm) and the external thread pitch diameter are intentionally machined to adjusted baselines so that deposit buildup falls within specification after plating. Calibrated 6g go and no-go thread gauges are used to verify fit before and after surface finishing. Furthermore, a post-plate de-embrittlement baking process is applied to prevent hydrogen embrittlement, ensuring that the 72-hour neutral salt spray corrosion resistance is achieved without compromising assembly clearances or torque consistency.
TEL: +86 187 5714 8656
Email: zhouli@chinaliqin.com
WhatsApp:+86 187 5714 8656
Website:https://www.cncliq.com/