 English



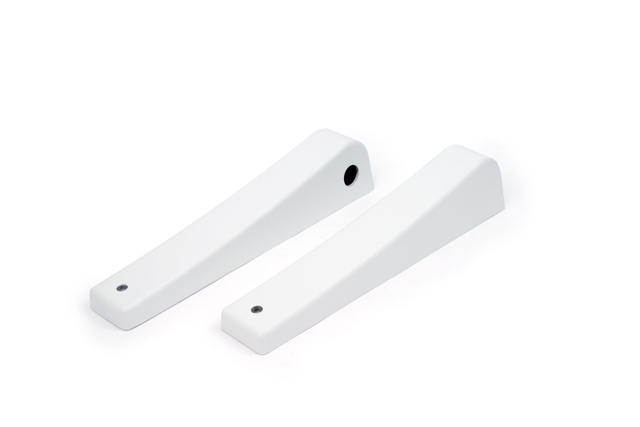
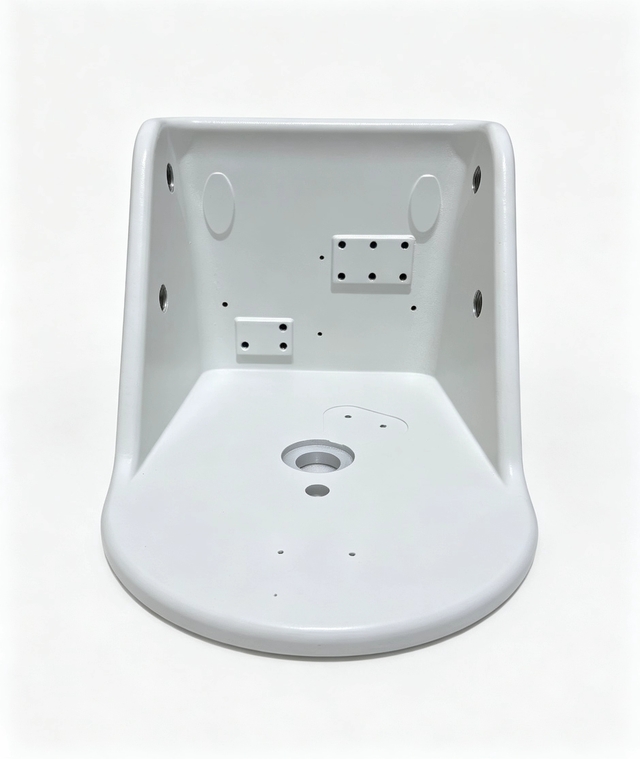
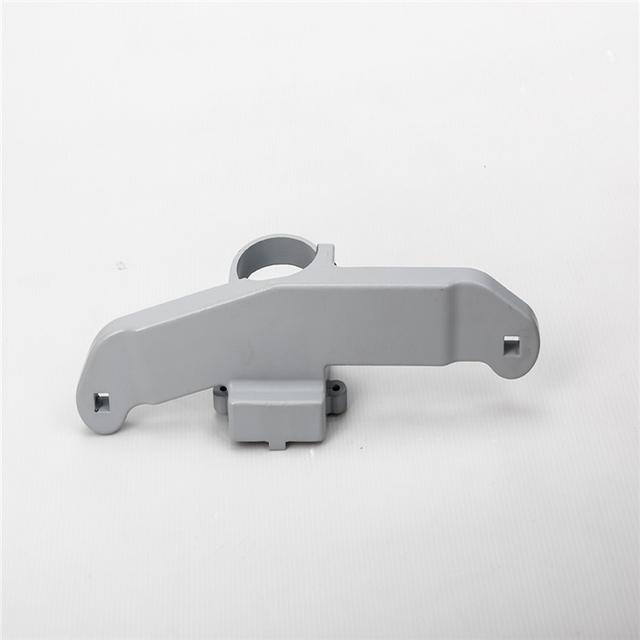
Product Description
| thing | describe |
|---|---|
| Design/Size | According to customer's drawings or samples |
| Material | Aluminum: 6061, 6063, 6082, 7075, 5052, A380, etc.
|
| process | CNC machining, turning, milling, stamping, turning, cutting, etc. |
| Delivery time | Samples usually take 3-7 working days, and mass production will be carried out according to the detailed quantity after sample approval. |
| Surface treatment | Transparent anodizing, color anodizing, chemical coating, brushing, passivation, polishing, chrome plating, sandblasting, laser engraving, zinc plating, black oxide, nickel plating, chrome plating, carburizing, heat treatment, painting |
| Test equipment | Coordinate measuring machine (CMM), 2D measuring instrument, projector, altimeter, micrometer, thread gauge, hardness tester, caliper, pin gauge, salt spray tester, concentricity measuring instrument, spectrometer. |
| Quality Management System | ISO 9001:2015
|
| application | Auto parts, machinery parts, computer parts, medical parts, home appliance parts, electrical parts, electronic product parts, electronic parts, generator parts, alternator parts, generator parts, stationery, power switches, micro switches, construction, merchandise and A/V equipment. |
| File Format | Solidworks, Pro/Engineer, CAD, PDF, JPG, DXF, IGS |
| Package | Inner plastic bag, outer standard carton, or as per customer's requirements |
| Shipping | Sea freight, air freight, international express (DHL, FedEx, TNT, UPS). |
| Serve | The professional foreign trade team provides enthusiastic and fast response services.
|
1. Executive Summary and Design Intent
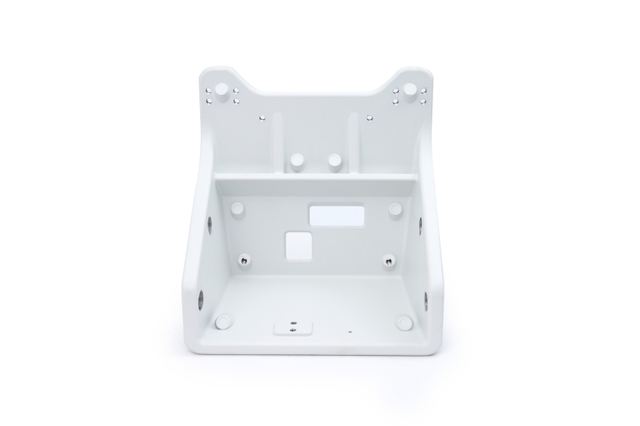
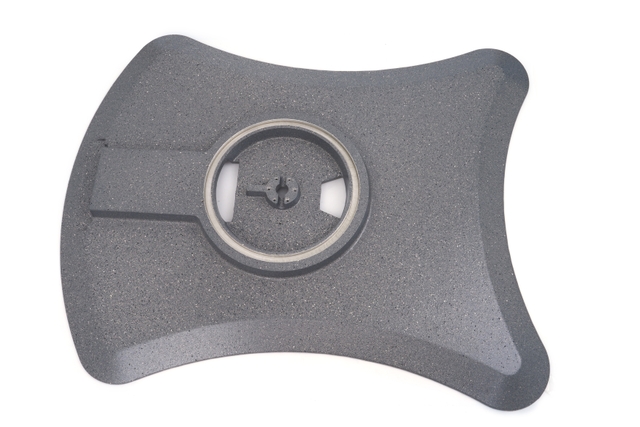
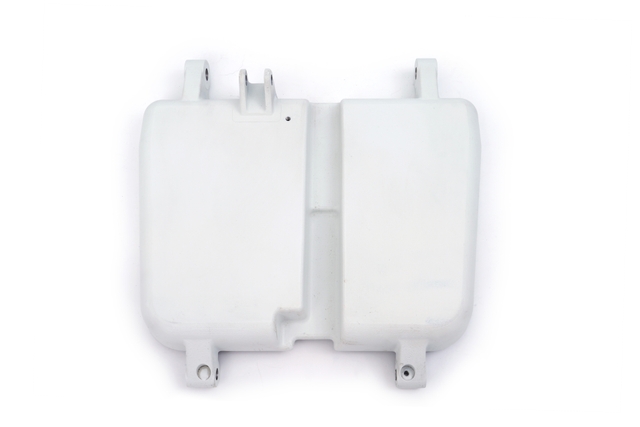
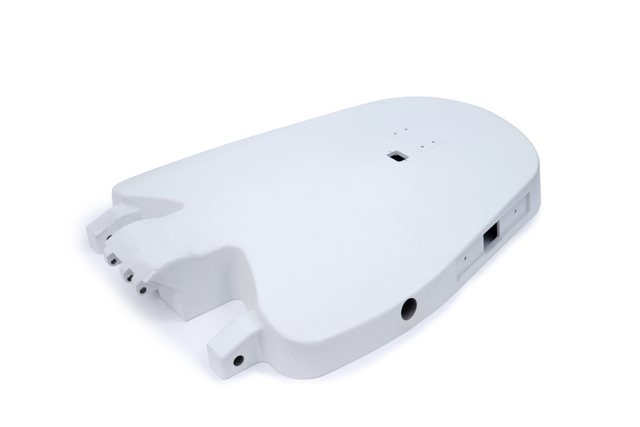
Modern dental operatory workstations represent a synthesis of ergonomic comfort, structural endurance, and dynamic positioning. At the structural core of this clinical environment lies the Upper Base, an integral chassis component designed to carry, articulate, and stabilize the patient examination chair. Positioned strategically within the dental chair linkage mechanism, this component serves as the central junction between lifting hydraulic/electromechanical actuators, tilt mechanisms, and peripheral support assemblies.
Because dental procedures require absolute positional stability during delicate microscopic endodontics, implant surgery, and periodontal treatments, zero positional deviation and high vibration dampening are critical functional criteria. This upper base meets these challenges through structural rib reinforcement, optimized internal cavity routing, and balanced mass distribution.
2. Advanced Material Engineering: A356-T6 Aluminum Alloy
The physical foundation of this base is engineered from premium-grade A356 aluminum alloy, cast and subsequently subjected to standard T6 solution heat treatment and artificial aging.
-
Strength-to-Weight Optimization: While traditional healthcare hardware historically relied on heavy cast iron or fabricated carbon steel plates, A356-T6 alloy delivers high mechanical yield strength and tensile resilience with nearly one-third the bulk density. This significantly reduces moving inertia during height and tilt adjustments without sacrificing structural rigidity.
-
Vibration Attenuation: Dental handpieces, scaler motors, and floor pumps introduce low-frequency mechanical waves into the operatory equipment. The crystalline matrix of aged A356 aluminum absorbs and dissipates structural vibration, ensuring that doctors maintain tactile steadiness and patients remain relaxed.
-
Internal Integrity and Creep Resistance: The microstructure developed during controlled heat treating eliminates residual internal casting stresses, mitigating warping, dimensional drift, or progressive material fatigue over decades of continuous duty cycles.
3. State-of-the-Art Machining and Manufacturing Process
Transforming the raw structural casting into a finished, ready-to-mount component requires rigorous subtractive manufacturing across high-speed multi-axis CNC machining centers.
-
First Operational Setup (Machining Center 1 - Datum Registration and Base Milling):
The raw casting is aligned to primary registration points to mill the primary reference planes, keeping overall planarity within a controlled 1.52-millimeter flatness tolerance across extended mounting surfaces. Outer wall symmetry is held with wall thickness deviations below 1.0 millimeter. In the same clamping phase, 12 precision 3/8-16 UNC-2B through-holes are drilled, counterbored, and roll-tapped with high-precision metric tooling.
-
Second Operational Setup (Machining Center 2 - Heavy Pivot Bores):
The secondary operational phase focuses on the side pivot journals, which bear dynamic cantilever loads during chair movement. Four heavy-duty 1-1/8-12 UNF-2B tapped holes with ø26.6-millimeter pilot diameters are line-bored from opposite sides. Multi-axis synchronization maintains concentricity across both flanks, holding bilateral center-line offset within 0.5 millimeter.
-
Third Operational Setup (Machining Center 3 - Auxiliary Detents and Sensor Bosses):
Final cutting paths mill complex wire clearance pass-through pockets, secondary stop brackets, and fine-thread auxiliary mountings (including 2 blind 3/8-16 UNC holes to 16.5-millimeter thread depth and specialized 10-32 UNF-2B sensor-mounting positions with controlled 6.35-millimeter effective threading depth).
4. Surface Finishing and Aesthetic Protection
Medical hardware must endure stringent clinical infection control protocols, involving continuous wiping with aggressive chemical agents and disinfectants.
-
Dual-Action Mechanical Sanding (DA Sanding):
Prior to surface coating, every external surface undergoes dual-action mechanical prep sanding. This eliminates parting lines, tool transition witness marks, and sharp outer edges, resulting in rounded edges that are safe for technicians and clean-room compliant.
-
Precision Thread Masking:
Before powder application, dedicated high-temperature masking caps, tapered silicone plugs, and custom sleeves seal every internal thread, including all 10-32 UNF, 3/8-16 UNC, and large 1-1/8-12 UNF tapped bores. This ensures that mating hardware threads effortlessly during downstream assembly with zero thread chase required.
-
Electrostatic Snow-White Medical Powder Coating:
The part is electrostatically powder coated using medical-grade snow-white thermoset powder. The oven-cured coating forms a pore-free, chemical-resistant barrier that resists scratching, chipping, impact deformation, and discoloration caused by prolonged UV or disinfectant exposure. The interior accommodates controlled overspray while maintaining clean functional internal cavities.
5. Systematic Quality Assurance and Verification
Dimensional integrity and structural consistency are validated across the entire production run:
-
In-Process Statistical Inspection: Manufacturing quality gates mandate regular checks every 2.5 hours per operating CNC machine, with at least 1 piece measured per cycle, and critical functional features verified across 3 consecutive pieces.
-
Dual-Method Metrology:
-
Precision go/no-go plug and thread gauges verify thread pitch, thread class engagement, and entry countersinks.
-
Specialized Coordinate Measuring Machines (CMM) run dedicated inspection routines to evaluate complex geometric dimensioning and tolerancing (GD&T) profiles, hole-pattern alignments, and true positions across internal structural faces.
-
Grade-00 inspection surface plates paired with calibrated dial indicators verify plane flatness and edge squareness.
-
6. Application Environment and Assembly Integration
-
Sub-Chassis Integration: This upper base component is engineered to sit directly within the primary articulating linkage of modern dental chairs, acting as the structural bed for the seat frame, cantilever backrest joints, and instrument delivery arm brackets.
-
Integrated Cable Harness Management: Internal routing apertures and chamfered clearance cutouts allow hydraulic hoses, vacuum lines, fiber-optic delivery tubing, and digital control wiring to pass cleanly through the center of rotation. This internal management eliminates pinch points and external harness clutter, protecting vital electrical and fluid paths during dynamic chair articulation.
7. Distinct Competitive Advantages
-
Superior Dynamic Load Distribution: Finite element-optimized wall thickness and built-in vertical gussets distribute dynamic loading across the entire casting body, suppressing localized stress points when patients lean or shift weight.
-
Smooth Mechanical Articulation: Accurate center-line alignment of the opposing 1-1/8-inch pivot sockets prevents bearing bind and uneven friction, allowing mechanical links to cycle quietly without jerkiness or mechanical chatter.
-
Corrosion Resistance and Clinical Cleanliness: Non-ferrous metallurgy combined with a tough, non-porous powder barrier creates an environment hostile to bacterial accumulation, resisting washdowns with ethanol, isopropyl, or sodium hypochlorite solutions.
-
Assembly-Line Ready: Delivered with pre-tested threads, deburred edges, clean mounting cavities, and zero residual machining chips, the component slots directly into clinical assembly lines without rework or manual chasing.
8. Long-Term Customer and Commercial Value
Integrating this engineered upper base into modern dental operatory chair designs delivers measurable commercial returns:
-
Elevated Brand Reputation: A smooth, whisper-quiet, jitter-free chair movement enhances patient comfort, reinforcing the premium market reputation of the dental brand.
-
Reduced Total Cost of Ownership (TCO): Eliminating mechanical fatigue and bore distortion avoids premature field failures, reducing warranty claims and technical service calls.
-
Optimized Production Throughput: Uniform casting dimensions and clean threaded interfaces ensure repeatable assembly fits, speeding up line cycle times and accelerating product delivery schedules.
FAQ
Q1: Why is A356-T6 cast aluminum preferred over conventional cast iron or welded steel structures for this component?
A: Dental operatory chairs demand exceptional motion smoothness, acoustic silence, and responsive elevation dynamics. Compared with heavy cast iron or fabricated weldments susceptible to thermal warpage, heat-treated A356-T6 aluminum combines high structural rigidity with low mass density, markedly cutting dynamic inertia and extending the service life of lifting actuators. Furthermore, the inherent internal damping characteristics of aged aluminum suppress high-frequency mechanical vibrations from drive motors, while eliminating the long-term risk of internal oxidation or rust in moisture-prone operatory environments.
Q2: How are threaded hole tolerances and mounting surface accuracies preserved after electrostatic powder coating?
A: We apply a strict multi-tier masking and surface preparation protocol across every manufacturing batch. Before the electrostatic coating stage, all critical tapped holes—ranging from 10-32 UNF auxiliary bosses to heavy 1-1/8-12 UNF pivot bores—are mechanically isolated using high-temperature silicone plugs and custom caps to prevent overspray deposition inside internal threads. Additionally, dual-action rotary sanding removes all tooling witness marks and parting lines prior to painting, ensuring full hardware interchangeability and allowing immediate, chase-free assembly right out of the shipping crate.
Q3: How does the structural design accommodate dense utility routing while managing high dynamic mechanical loads?
A: The base serves as both a primary load-bearing chassis and a centralized utility management junction within the operatory chair. Its engineered open-cavity architecture features smooth-edged cutouts that separate and route water tubing, suction lines, air supply, and electrical harnesses without pinch points or chafing during articulation. Structurally, integrated internal stiffening ribs reinforce the casing against torsional deflection, while synchronized line-boring across bilateral pivot journals balances cantilever moments, guaranteeing shake-free positioning even under maximum patient working capacities.
Our Core Advantages
- Specialized process solutions for medical mechanical parts, fully familiar with strict medical standards on cleanliness, corrosion resistance and burr-free surfaces. Support compliant custom processing for medical device manufacturers.
- Full in-house clean manufacturing including milling, tapping, cleaning and powder coating without outsourcing, shortening lead time for prototypes & mass orders.
- Complete precision testing equipment including CMM, thread gauges, film thickness meters & salt spray testers. Full sets of dimensional, salt spray and cleanliness reports can be supplied.
- One-stop customization: drawing optimization, material replacement, clean process adjustment & fast prototype sampling, matching small-batch & repeated orders of medium & small medical equipment factories.
We specialize in non-standard precision structural components for medical devices. With strict clean production control and mature manufacturing systems, we supply durable bottom load-bearing base components for automatic medical testing and pharmaceutical production lines.
TEL: +86 187 5714 8656
Email: zhouli@chinaliqin.com
WhatsApp:+86 187 5714 8656
Website:https://www.cncliq.com/