 English




A buyer once asked our shop a question that sounded simple: “Can we switch this visible extrusion from 6063 to 6061 so the mounting tabs are stronger?” The answer was not a quick yes or no. The profile had thin fins, a long cosmetic face, four post-machined holes, and a clear anodized finish that had to match the surrounding frame. More strength in the material data sheet could easily create a harder extrusion job, more die lines, slower press output, and a less forgiving cosmetic result.
That is the real 6063-versus-6061 decision. It is not a contest to find the “better” aluminum. It is a routing decision: which alloy gives the drawing the best path through extrusion, CNC machining, finishing, inspection, and assembly? This guide explains that path from a shop-floor point of view. If you release drawings or buy parts for a living, this is for you. The target is repeatable hardware, not a pretty comparison sheet.
Short answer: Here is how it usually shakes out on the shop floor. Loads, threads, and lots of post-machining steer us toward 6061. A skinny, complicated section that customers will see after anodizing normally puts 6063 at the front of the line. If one part needs both, do not guess. Review the temper, profile geometry, machining datums, surface class, and final coating callout together.
6063 vs 6061 at a Glance
|
Decision point |
6061 aluminum |
6063 aluminum |
Practical sourcing meaning |
|
Typical reason to specify it |
Higher structural strength and versatile CNC fabrication |
Better extrudability and a cleaner decorative surface |
Start with function, then verify appearance and process route |
|
Common extruded tempers |
T6, T6510, T6511 |
T5, T52, T6 |
“6061” or “6063” alone is not a complete RFQ specification |
|
CNC behavior |
Generally firmer and easier to control for accurate post-machining |
Machines well with sharp aluminum geometry but can feel softer or gummier |
Tool edge, chip evacuation, fixture support, and temper can matter more than the alloy name |
|
Profile extrusion |
Suitable for stronger, less intricate profiles |
Preferred for intricate, thin-wall, high-finish profiles |
6063 usually gives the die designer a wider processing window |
|
Decorative anodizing |
Good when the lot and pretreatment are controlled |
Usually more uniform and brighter on visible extrusions |
Approve a boundary sample; never use “black anodize” as the entire appearance spec |
|
Best-fit examples |
Machine frames, brackets, fixtures, structural housings, threaded components |
Display frames, trim, heat-sink profiles, rails, visible enclosures, complex tubing |
Useful screen, not a verdict—the drawing and the real duty cycle still get the last word |
Look beneath the grade stamp and both alloys sit in the heat-treatable 6xxx family. Magnesium and silicon do most of the strengthening work. The permitted ranges overlap on paper; even so, 6061 is the grade normally called on when the designer needs more strength. 6063 deliberately trades some strength for easier metal flow and a better finishing response. Hydro’s published 6063 extrusion data sheet rates 6063 highly for surface finish and decorative anodizing, while its 6063 alloy overview notes that heavier machining and structural loads often point toward 6061. That is useful industry consensus, but the certificate for the actual lot still governs the part.
Why Alloy and Temper Must Be Chosen Together
A frequent RFQ mistake is a drawing note that says only “Aluminum 6061” or “Aluminum 6063.” Temper is not a footnote. We feel it at the press, at the straightener, under the cutter, and again when an unclamped part decides whether to stay put. Take a 6063-T5 display rail and a 6063-T6 machined tube. Same alloy family, quite different expectations for strength and cutting. The last digits matter on 6061 too: T6511 identifies a stretched, stress-relieved extrusion, often welcome when a long part will be milled harder on one side than the other.
When the purchase covers an extruded bar, rod, profile, or tube, ASTM B221 is a common North American reference. Open it and you will find the chemistry and mechanical-property requirements tied to the listed alloys and tempers. European drawings commonly work with EN 755 series requirements, and precision 6060/6063 profiles may invoke EN 12020. Put the applicable standard on the purchase order. Then state the temper, profile drawing revision, required inspection document, and whether dimensional acceptance occurs before or after anodizing.
One strength figure lifted from a web chart is a poor release criterion. Change the temper, section thickness, product form, or governing standard and the applicable minimum can move. During concept work, it is fair to say 6061-T6 is clearly stronger than 6063-T6. Once the drawing is released, though, go back to the correct table and the certificate for that exact section.
Machinability at the Spindle: Where the Difference Shows Up
Both alloys machine comfortably on a capable CNC, but they fail in different ways. A well-aged 6061 extrusion usually feels more supportive under the tool. That makes it a comfortable shop choice for bearing seats, threaded bosses, counterbores, and load-carrying interfaces. The recipe is not exotic: polished flutes, positive rake, a real chip load, and enough coolant or air to get the chips out. Set those basics correctly and edges stay sharp while dimensions behave.
6063 is not “unmachinable.” Far from it. We regularly treat it as a profile that needs accurate secondary operations rather than a billet that wants aggressive stock removal. Its lower hardness can encourage built-up edge if the tool rubs, dwells, or recuts warm chips. The result may be a smeared edge, a cloudy face, or a burr that becomes painfully obvious after anodizing. Keep the edge sharp. Give the chip somewhere to go. Support thin walls close to the cut instead of clamping harder and bending the section.
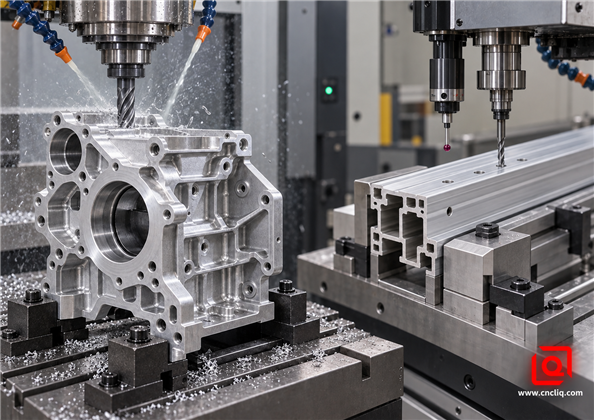
Secondary machining should be planned around section stiffness, datum quality, chip evacuation, and the final visible surface.
Four machining controls that matter on both alloys
1. Start from stable datums. Raw extrusion faces can carry crown, twist, bow, die lines, or local variation. Locate from a supported wall, a designed tooling feature, or pre-machined pads. Long profiles often benefit from probing rather than a hard stop that assumes perfect straightness.
2. Use aluminum-specific cutting geometry. A sharp polished tool with a generous flute space reduces adhesion and chip packing. A coating chosen for steel can round the edge and make a soft aluminum cut worse; thin ZrN or DLC may be considered when the tool strategy requires a coating.
3. Finish after the part has relaxed. Heavy, one-sided material removal can release residual stress. Rough first, release or re-seat the part, then finish critical interfaces. The exact sequence depends on section length, temper, stock condition, and tolerance—not a universal waiting-time recipe.
4. Deburr for the coating, not only for touch. A feather burr at a hole, slot, or edge can survive casual inspection and then brighten, burn, or trap chemistry during anodizing. Define edge breaks and protect the cosmetic face during every transfer.
For a deeper process discussion, Liqin’s guide to aluminum CNC milling, turning, and extrusion post-machining explains why profile straightness, probing, and chip control belong in the same process plan. Does the drawing contain a bore or slide that is accepted only after coating? In that case, continue with Liqin’s guide to machining allowances for anodized aluminum is the more relevant next step.
RFQ checkpoint: A useful package has the 3D model and the controlled 2D drawing. Add annual quantity, proposed alloy and temper, a cosmetic-face map, the anodize callout, and the mating fit. With that in hand, Liqin can put 6061, 6063, and a hybrid extrusion-plus-CNC route side by side before anyone releases tooling. Request a drawing-based DFM review.
Anodizing: The Finish Starts Before the Tank
6063 has earned its “architectural aluminum” reputation because it can extrude with a smooth surface and respond consistently to decorative anodizing. Lower copper and controlled impurity levels help. On a long visible rail or enclosure bezel, that cleaner baseline matters. Clear, champagne, bronze, or black finishes expose everything beneath them: die pickup, handling rub, coarse grain, weld zones, aggressive sanding, and mismatched material lots.
6061 also anodizes well. It is widely used for black and natural anodized machined parts. The caution is not that 6061 automatically looks bad; the caution is that structural choice and cosmetic promise must be managed together. A machined face and an untouched extrusion face may etch differently. Two melt lots can land on slightly different shades. A welded region can reveal a halo. A polished logo panel may no longer match a bead-blasted mounting boss.
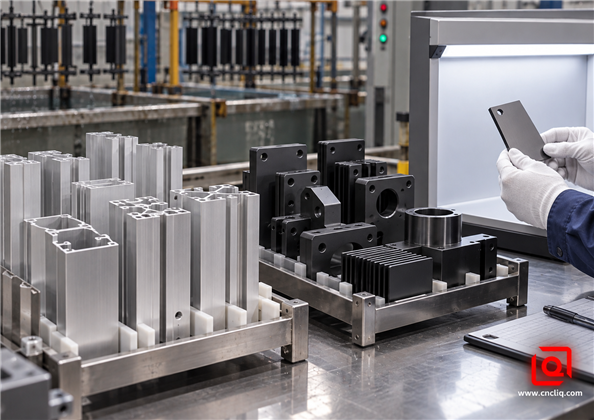
A boundary sample, one material lot, controlled pretreatment, and agreed viewing conditions do more for color consistency than a vague color name.
Specify the appearance in a way a factory can inspect
· Mark cosmetic faces and non-cosmetic faces on the drawing.
· Name the anodizing standard and coating class. ISO 7599:2018, confirmed current in 2023, covers how decorative and protective anodic coatings are specified and highlights the importance of alloy grade and pretreatment to final appearance.
· State color, gloss or texture expectation, sealing requirement, and any corrosion or wear test.
· Define an approved limit sample or range rather than promising an impossible perfect visual match across unrelated lots.
· Identify contact points and racking marks. Electricity needs a contact, so “no marks anywhere” is not a workable instruction.
· Call out masked threads, ground faces, electrical contacts, bearing seats, and other no-coat zones.
Anodizing also changes size. The coating is formed partly into the base metal and partly outward, but the exact dimensional change should come from the approved process and coating specification. For a precision bore, thread, sliding rail, or seal land, do not apply a generic internet “50/50 rule” and release the drawing. Agree the finish thickness, masking plan, pre-coat target, measurement method, and final acceptance dimension with the manufacturer and anodizer.
For general decorative work, 6063 gives the finishing team a friendlier starting surface. For hard-working machined parts, 6061 often gives design and machining teams the stronger overall package. Sometimes the cleanest answer is to stop asking one alloy to do two jobs. Keep the visible rail in 6063. Put 6061 where the load actually enters. Then detail the joint so a shade change is controlled—or looks deliberate.
Extrusion Quality: Why 6063 Gives the Press More Room
Picture what the press is being asked to do. Hot metal must divide, turn, squeeze through the die, join again in a hollow section, and repeat that act for meters. 6063 usually flows with less argument than 6061. Thin walls, skinny slots, internal chambers, and small visible details therefore have a better chance of running cleanly. Press speed may improve and poor fill may fall, but that is not a price promise. Size, die difficulty, tolerances, tool life, volume, and every operation after the saw still sit on the quotation.
6061 can be extruded, and it is the right answer for many structural profiles. It simply asks more from the press and die when the section becomes intricate. Trouble starts when 6061 is chosen for strength but drawn like a wispy 6063 trim. Abrupt wall changes, delicate die tongues, and deep narrow pockets do not disappear because the CAD section looks elegant. The extruder has to price that headache. Over a long program, a slightly heavier and better-balanced 6061 section can beat a clever profile that never runs calmly.
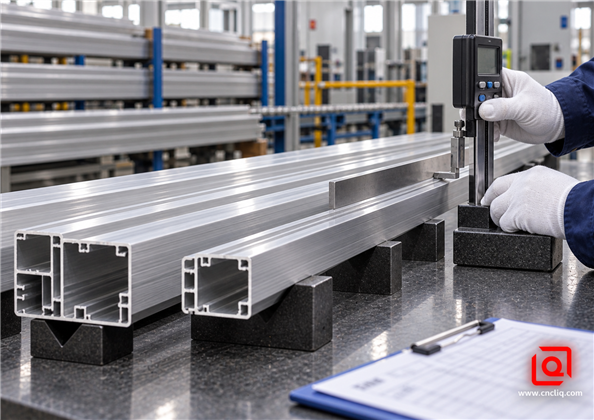
A cut-length check is not incoming inspection. Lay the profile out, look down its length, measure the section, inspect the finish, confirm the temper, and ask whether CNC has a datum it can actually trust.
Defects that travel downstream
|
Observed condition |
Why it matters after extrusion |
Control before CNC or anodizing |
|
Bow or twist |
Creates inconsistent seating, hole position drift, and variable clamp load |
Define applicable straightness/twist acceptance; inspect on a suitable support; probe long parts where needed |
|
Die lines or pickup |
Can remain visible through clear or color anodizing |
Assign a cosmetic surface class; maintain the die; approve a representative anodized sample |
|
Wall-thickness imbalance |
Changes stiffness, cooling, aging response, and machining deflection |
Balance the section where possible; identify truly critical walls instead of over-tolerancing every feature |
|
Seam or weld-line sensitivity in hollow profiles |
May affect appearance or performance depending on location and duty |
Review die concept and seam location with the extruder; apply any required testing from the product specification |
|
Mixed lots or tempers |
Can create shade, hardness, and machining variation |
Maintain material traceability and segregate lots for matched visible assemblies |
|
Handling damage |
Small rub marks often become obvious after chemical pretreatment |
Use separators, clean gloves, protected racks, and defined packaging from press to finish |
This is why a profile drawing should not be evaluated in isolation from the post-operations. Liqin’s comparison of full CNC machining versus an extrusion-plus-machining route is useful when a constant cross-section can replace large amounts of billet removal. It also explains the datum problem that appears when a raw profile is treated as if it were a precision-machined block.
Which Alloy Fits Your Part?
|
Part requirement |
Likely starting choice |
Reason |
Question to resolve before release |
|
High-load machined bracket with tapped holes |
6061-T6/T651 variant |
Higher strength and robust general machinability |
Is stock form and stress-relieved temper appropriate for the material-removal pattern? |
|
Visible thin-wall enclosure rail |
6063-T5 or T6 |
Good metal flow and decorative finish potential |
Which faces are cosmetic, and what post-machined features need final tolerance? |
|
Complex heat-sink extrusion |
6063 as the first DFM study |
Intricate fins and surface consistency often dominate |
Does the thermal and mechanical model truly need 6061 strength? |
|
Long structural machine member |
6061 as the first DFM study |
Load and attachment features can outweigh finish |
Can the section be simplified enough for stable extrusion and straightening? |
|
Premium black-anodized front panel |
6063 if primarily extruded; 6061 if heavily machined |
Route depends on visible area, stiffness, and cut features |
Can one lot, one pretreatment route, and a boundary sample be maintained? |
|
Prototype with uncertain geometry and low volume |
6061 billet or standard profile |
Avoids committing to a dedicated extrusion die too early |
At what validated volume does custom extrusion become economical? |
There is one more trap: a part controlled by deflection. The elastic modulus of these aluminum grades is broadly similar. Keep the geometry unchanged and a switch to 6061 will not suddenly turn a flexible rail into a rigid beam. If deflection rather than yielding controls the design, changing wall placement or section shape may do more than changing between these two alloys. Run the load case before paying for strength the part never uses.
Verified Product-Based Case: 6061-T6 Preform Plus Precision CNC
The following example is based on a published Liqin product and is presented without customer identity or unverified order metrics. It is useful because it shows where 6061 earns its place—and also why “extrusion” must be defined correctly.The part is a 6061-T6 lightning-arrester electrode produced from a cold-extruded preform and precision CNC machining. Cold extrusion is a discrete forming process, not the continuous hot-profile extrusion used for long rails and frames.
The product has small symmetrical structures, slots, cavities, holes, threads, and close-fitting features. Liqin’s published route begins with qualified 6061-T6 bar preparation, then forms the main blank in a dedicated cold-extrusion die. Post-forming work includes stress management, datum preparation, light clamping in a dedicated fixture, CNC finishing, hole and thread machining, detailed deburring, and dimensional inspection. The product page specifically identifies micro-deformation, blank-to-fixture positioning, die wear, and consistent tiny-feature filling as manufacturing concerns.
Why not turn this into a generic claim that 6061 is always superior? Because the route answers a different problem. Here the component needs an integrated near-net preform and accurate functional details; decorative long-profile surface quality is not the main driver. A 6063 architectural profile would not solve the geometry. The correct lesson is broader: choose the alloy and forming route as a pair, then design the CNC datums around the real blank condition. That is the same discipline required when post-machining a hot-extruded 6063 housing.
Have a similar make-or-buy decision? Share the annual volume, drawing, material requirement, finishing callout, and the surfaces that drive assembly. Liqin can compare billet machining, standard profile, custom hot extrusion, cold extrusion, and downstream CNC without forcing every part into one process. Send your RFQ for a process-route review.
How to Write an RFQ That Produces a Useful Quote
A strong RFQ lets the supplier price the risk instead of guessing at it. Include these items:
· Alloy, temper, and standard: for example, AA 6063-T6 to the agreed extrusion standard—not simply “aluminum.”
· 3D and controlled 2D files: the 3D model communicates shape; the drawing defines datums, tolerances, threads, finish, and inspection.
· Product form: billet, plate, standard extrusion, custom hot-extruded profile, or cold-extruded preform.
· Quantity profile: prototype quantity, first production batch, annual demand, and expected program life.
· Cosmetic map: A/B/C surfaces, grain direction, handling limitations, permissible rack marks, and boundary sample requirement.
· Anodizing details: standard, type/class, thickness range, color, texture, seal, tests, masking, and final dimensional acceptance.
· Functional interfaces: mating parts, bearing or seal fits, electrical contact zones, and features measured after finishing.
· Documentation: material certificate, first-article report, inspection format, traceability, and any regulatory requirements.
If the section is not frozen, ask for DFM before the die is cut. Moving a rib, evening a wall transition, opening a narrow channel, or adding a sacrificial locating feature may improve press stability and simplify machining. These changes are inexpensive in CAD and expensive after tooling approval.
Cost: Look Beyond Price per Kilogram
6063 is often cheaper to push through a complex die, while 6061 may reduce section size when strength governs. That does not make either alloy universally cheaper. The landed part cost includes billet premium, die investment, press time, scrap, heat treatment, straightening, cutting, fixtures, CNC cycle time, deburring, anodizing yield, inspection, packaging, and freight.
For low volume or changing geometry, standard 6061 stock and CNC machining can be the sensible route because it avoids dedicated tooling. Once the cross-section stabilizes and volume grows, a custom 6063 profile may remove most rough machining and expose a better cosmetic surface. Conversely, a heavily loaded profile may justify 6061 even if extrusion runs more slowly. Ask suppliers to quote the complete route and identify assumptions. A cheap extrusion that creates extra straightening, cosmetic scrap, or five-axis rework is not a cheap part.
Frequently Asked Questions
1. Is 6061 always easier to machine than 6063?
6061 is generally the easier starting point for structural CNC work because it is stronger and often less gummy, but the actual result depends on temper, stock form, section stiffness, tool geometry, chip evacuation, and clamping. A stable 6063-T6 profile with sharp polished tooling can machine beautifully, while a stressed or poorly supported 6061 extrusion can move after release.
2. Does 6063 always look better after anodizing?
6063 is normally preferred for decorative anodized extrusions because its chemistry and extrusion response support a smooth, consistent finish, but alloy alone cannot guarantee appearance. Die condition, grain structure, melt lot, handling, machining marks, pretreatment, racking, bath control, and sealing all influence the result, so visible assemblies should use controlled lots and an approved boundary sample.
3. Can 6061 be used for complex extruded profiles?
Yes, 6061 is widely extruded, particularly for structural members, but very thin walls, deep pockets, narrow openings, and abrupt thickness changes can make the press and die work harder than they would with 6063. The extruder should review circumscribing size, wall balance, tongue ratio, seam location, tolerance, temper, and cosmetic class before the profile is released.
4. Which alloy should I use for an anodized heat sink?
6063 is the usual first candidate for an extruded heat sink because fine fins, surface finish, and profile economics often drive the design, while 6061 deserves consideration when threaded attachments, impact, or higher structural loads dominate. Thermal performance also depends on fin geometry, airflow, interface resistance, and the coating, so confirm the full thermal and mechanical model rather than choosing by alloy name alone.
5. What should I send to receive an accurate 6061 or 6063 quote?
Send the STEP file and controlled 2D drawing, alloy and temper, applicable material standard, quantities, annual forecast, cosmetic-surface map, anodizing specification, masking zones, post-finish tolerances, inspection documents, target delivery, and any mating-part information that affects fit; if the alloy is not fixed, say so and request a side-by-side DFM recommendation.
Summary
6061 is the practical first choice for stronger, heavily machined, threaded, or structural aluminum parts; 6063 is the practical first choice for intricate profiles, thin walls, visible extruded surfaces, and consistent decorative anodizing. The safest decision comes from reviewing alloy, temper, section design, extrusion quality, CNC datums, cosmetic class, coating growth, and inspection as one manufacturing system. Send a complete drawing package before tooling release, approve a physical finish boundary, and make the supplier quote the whole route—not only the raw material.
Contact Information
Company: Ningbo Liqin Industry Co., Ltd.
Daily customer maintenance & after-sales support:service@shturl. zhuwanying@cncliq.com
New inquiry, quotation & order discussion:business@shturl. zhouli@chinaliqin.com
Hotline: +86 18757148656
Disclaimer
All technical articles, material specifications, machining recommendations, and surface treatment details published on this blog are for informational and reference purposes only. Please note that general blog insights do not replace signed technical agreements. Because custom parts vary by material heat numbers, machine calibrations, and specific tolerances, binding quality specs are governed solely by your approved CAD drawings, signed contracts, and formal quality plans.
All customer case studies featured on this blog have been thoroughly anonymized and sanitized. The performance metrics, manufacturing workflows, and imagery displayed serve solely to demonstrate our custom machining capabilities and do not represent a single universal standard for all orders.
Liqin Manufacturing Team
Built on 18 years of precision engineering experience, Ningbo Liqin Industry manufactures high-tolerance metal components for demanding global markets. We operate out of a 6,500 m² production hub equipped with over 150 machines, running 4-axis and 5-axis CNC machining, mill-turn machining, cold extrusion, and pressure die casting under one roof. This setup allows us to manage projects seamlessly, taking parts from initial CAD concepts directly to finalized shipments.
We handle quality control with zero compromise. We treat tight tolerances with the engineering discipline they require. Backed by ISO 9001, ISO 13485, and IATF 16949 certifications, our QA engineers run strict IPQC, FQC, and OQC checks on every single production batch. From CMM dimensional mapping and optical profiling to hardness and salt-spray testing, we validate your critical specs upfront—so you receive drop-in ready components with zero assembly headaches or costly line stoppages. On top of manufacturing, you can rely on us for two-hour response times on new RFQs, direct support for prototype sampling, and smooth export shipping across Europe, North America, Asia, and Oceania.
Welcome your inquiries and samples. Visit our website or contact us directly for a competitive quote!
